For OEM manufacturers, electrolytic copper wire is rarely a commodity line item. It is a specification-driven input whose grade, oxygen content, temper, and dimensional tolerance decide whether a downstream drawing, welding, or stranding operation runs at target yield. This review sets out what procurement and engineering teams should verify when sourcing high quality electrolytic copper wire for OEM projects, using the material classifications, process routes, and documentation practices that govern the copper industry.
Understanding the Copper Material Families
Copper materials are categorized by composition into two main groups: pure copper and copper alloys. Common alloys include brass (copper-zinc), bronze (copper-tin, copper-aluminum, and others), and cupronickel (copper-nickel). Based on oxygen content and deoxidation method, pure copper is further subdivided into tough-pitch copper (electrolytic tough-pitch copper), oxygen-free copper, and phosphorus-deoxidized copper. Oxygen content directly affects welding, formability, and resistance to hydrogen embrittlement, which makes it a key factor in material selection and technical inquiries.
- Pure Copper (Red Copper): High electrical and thermal conductivity; used for busbars, conductive components, heat exchangers, and water/gas piping. Representative grades: T1/T2/T3, TU1/TU2, TP1/TP2.
- Brass (Copper-Zinc Alloy): High strength, good machinability, golden-yellow appearance; used for tubing, hardware, valves, lighting fixtures, and connectors. Representative grades: H59–H80.
- Bronze / Cupronickel: Alloyed with tin, aluminum, or beryllium (bronze) or nickel (cupronickel); used for elastic components, wear-resistant parts, and applications in marine or corrosive environments.
- Specialized Conductive Forms: Copper busbars, braided copper wire and flexible connectors, and stranded copper wire; used for high- and low-voltage electrical equipment, switchgear, and transformer connections and grounding.
Common Grades and Chemical Compositions
Grade selection is the first control point, because the same nominal "copper wire" can span a wide composition range.
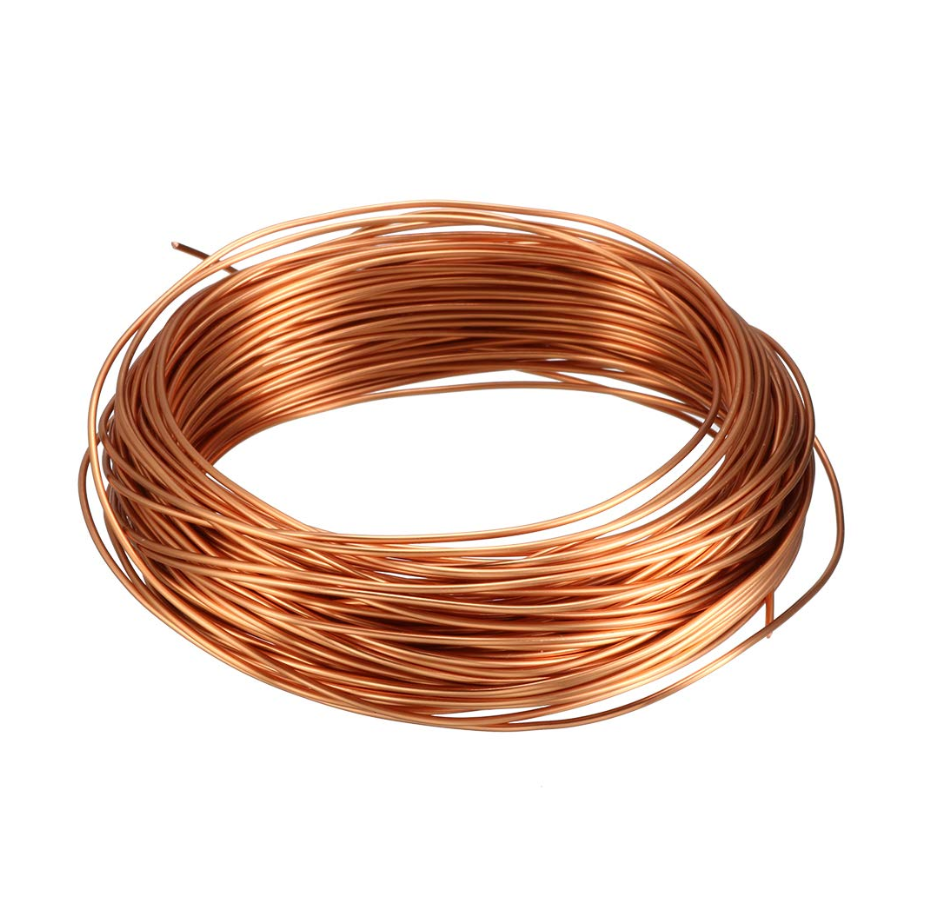
Pure copper (tough-pitch copper): T1, T2, and T3, with copper content decreasing sequentially — T1 ≥ 99.95%, T2 ≥ 99.90%, and T3 ≥ 99.70%. These are used primarily for general-purpose processed materials and electrical conductive components.
Oxygen-free copper: TU1 and TU2, characterized by high copper content and extremely low oxygen content (TU1 ≥ 99.97%, TU2 ≥ 99.95%); widely used in electronics, vacuum applications, and high-specification welded components.
Phosphorus-deoxidized copper: TP1 and TP2, both with copper content ≥ 99.90% and deoxidized via the addition of phosphorus (0.004%–0.040%). TP2 is the most commonly used grade, applied in water pipes, gas lines, heat exchangers, and air conditioning tubing.
Brass (copper-zinc alloy): copper content rises by grade — H59 (57–60%), H62 (60.5–63.5%), H65 (63–66%), H68 (67–70%), and H80 (79–81%), with the remainder being zinc. These alloys serve hardware, valves, profiles, deep-drawn parts, and decorative craft items.
Corresponding ASTM grades: C11000 is electrolytic tough-pitch copper (Cu ≥ 99.90%, equivalent to T2); C12200 is phosphorus-deoxidized copper (Cu ≥ 99.90%, equivalent to TP2). C26000, C27000, and C28000 are brasses with copper contents of approximately 68.5–71.5%, 64–67%, and 59–62%, roughly corresponding to H70, H66, and H60.
Identification key: Grade prefixes T, TU, and TP denote pure copper, while H denotes brass; the C-series indicates ASTM grades, where grades starting with C1 are typically pure copper and those starting with C2 are typically brass. Alloys with the same composition often correspond to both Chinese National Standards (GB) and ASTM designations — for example, TP2 ≈ C12200 and T2 ≈ C11000.
The Production Chain Behind Consistent Wire Quality
Copper product manufacturing generally begins with copper cathode (electrolytic copper) as the raw material and proceeds through smelting and casting, hot working, cold working, heat treatment, and final inspection and packaging:
- Raw materials — copper cathode/electrolytic copper with ≥99.95% copper content; qualified scrap may be blended in; batching is performed according to grade specifications.
- Smelting and casting — melting in induction or reverberatory furnaces; continuous casting and rolling or ingot casting. Phosphorus-deoxidized copper requires the addition of Cu-P alloy for deoxidation; controlling oxygen content is critical, since incomplete deoxidation risks porosity and hydrogen embrittlement.
- Hot working — heating billets or ingots above the recrystallization temperature; hot rolling for breakdown, extrusion into mother tubes or busbars, or piercing to form billets. Hot rolling at approximately 800–950°C breaks down as-cast dendrites, eliminates porosity, and refines grains.
- Cold working — cold rolling for thickness reduction, floating-mandrel or coil drawing for tube forming, and wire drawing for diameter reduction to control dimensional accuracy. Cold working causes work hardening, which necessitates alternating annealing steps.
- Heat treatment — intermediate annealing to restore plasticity; bright annealing or softening annealing to establish the final temper, followed by straightening and cutting to length. Annealing parameters directly determine the temper — soft, half-hard, or hard — and grain size.
- Inspection and packaging — testing for chemical composition, mechanical properties, electrical conductivity, flaw detection, dimensions, and surface quality; moisture-proof packaging and warehousing; mandatory standard-compliant sampling and retention of test reports for future reference prior to shipment.
Key Process Points for Copper Wire
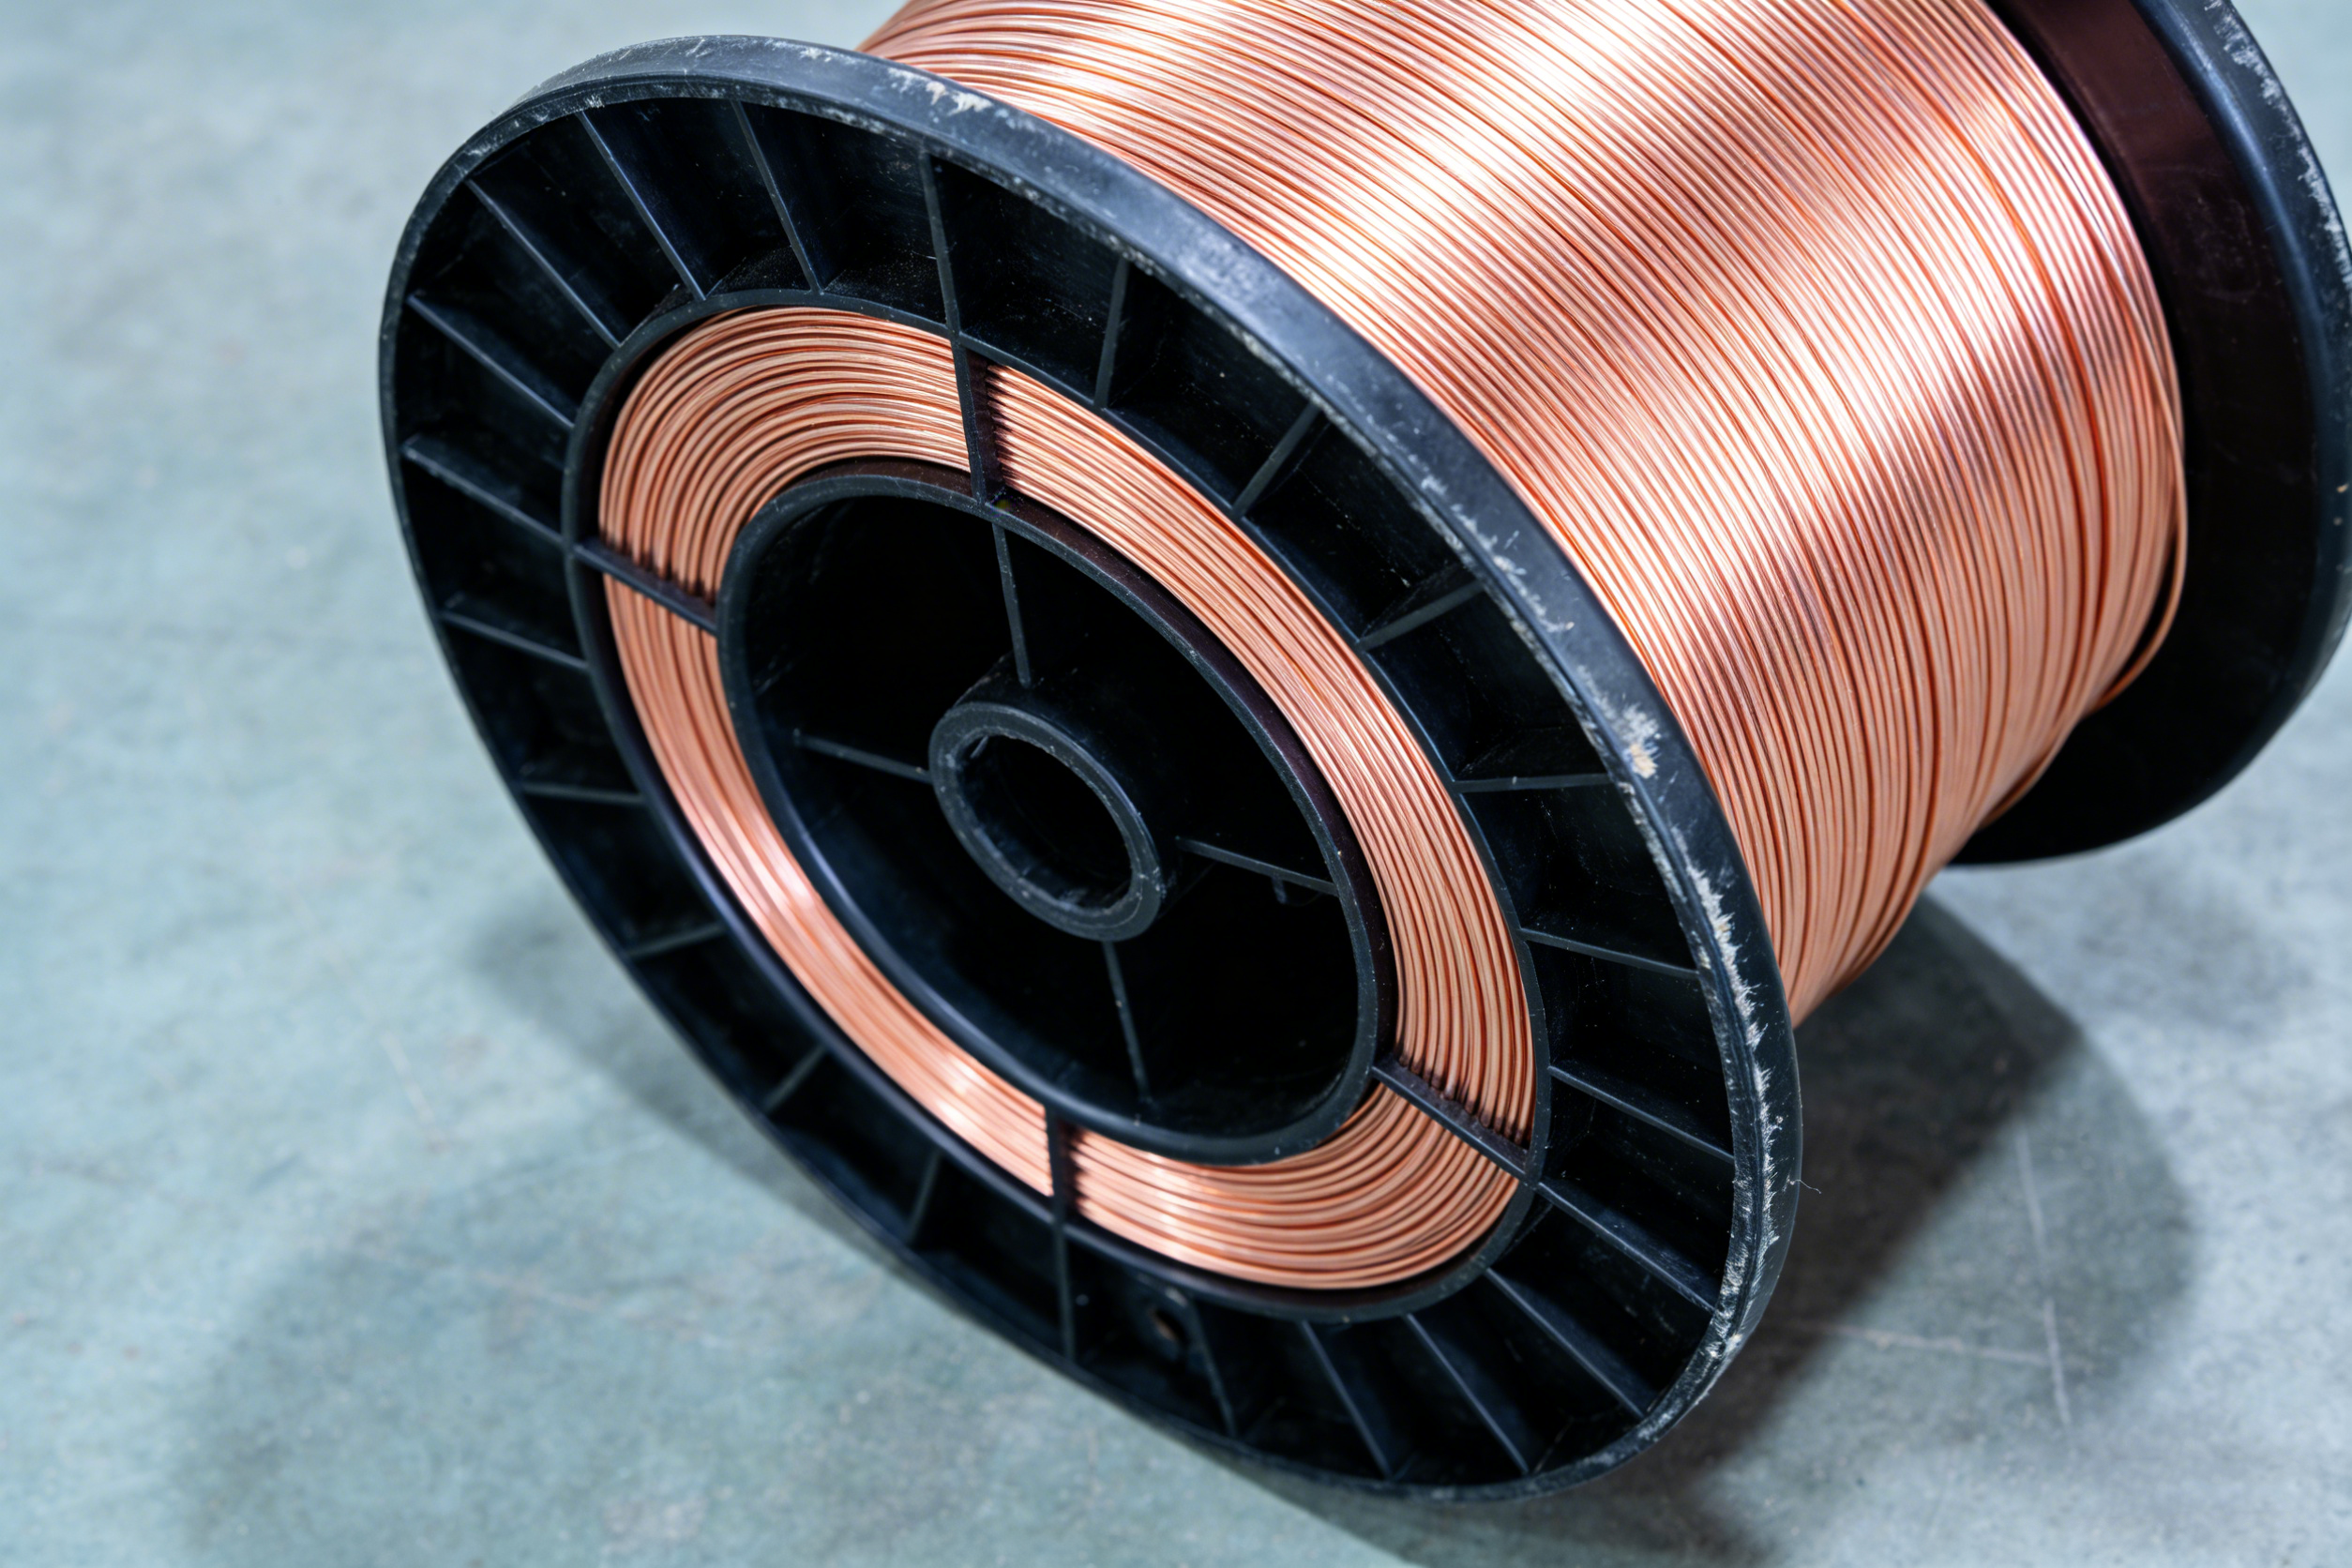
The process route for copper wire is wire drawing (multi-pass) → annealing → stranding/braiding. Key control points are wire diameter tolerance, electrical conductivity, wire breakage rate, and flexibility.
Adjacent product forms follow related routes. Copper tubes: melting and casting → extrusion or rotary piercing → cold drawing (coil drawing/floating mandrel) → annealing → straightening and finishing; key control points are wall thickness uniformity, inner surface cleanliness, and grain size in the annealed state, with air-conditioning tubes also requiring eddy current testing and hydrogen embrittlement testing. Copper busbars: copper cathode → melting → upward casting (rod) → extrusion → drawing → cutting to length → inspection; key control points include straightness (e.g., ≤ 0.5 mm/m), electrical conductivity, edge chamfering, and dimensional tolerances. Copper plates/strips: hot rolling (breakdown) → cold rolling → annealing → finishing (slitting/leveling). Braided copper wire and flexible connectors: stacking multiple layers of flat copper wires → braiding/extrusion → terminal crimping, where braid density, contact resistance, and terminal security are critical; flexible busbars often utilize multiple layers of 0.5 mm material with extruded insulation.
Temper Designations and Heat Treatment
- M (Soft Temper): Fully annealed/soft-annealed; high ductility and low strength; suitable for bending, flaring, and deep drawing. Common designations include T2M and H62M.
- M2 (Light Soft): Lightly soft-annealed; properties fall between soft and half-hard tempers; commonly used under the GB/T 1527 standard.
- Y2 (Half-Hard): Half-hardened by cold working; balances strength and ductility with good structural support. Designations include T2Y2 and H62Y2.
- Y (Hard Temper): Hardened by cold working; high strength and rigidity with lower formability. Designations include T2Y and H62Y.
- O60 (Air Conditioning Tube): Soft-annealed temper; a globally recognized designation commonly used in the air conditioning and refrigeration industries (e.g., TP2 O60).
Specification and Documentation Practices
For conductive busbars, the recommendation is pure copper busbars such as TMY/T2 or C11000, with electrical conductivity typically ≥ 46 m/(Ω·mm²) at 75°C and verified straightness. When requesting a quote, specifying the four key elements — "Grade + Temper + Cross-section + Standard" — keeps offers comparable.
Pricing for copper products follows a floating model of "LME/SHFE Copper Price + Processing Fee," so buyers should clarify both the pricing cycle and the method used to lock in the price (price-fixing).
Documentation is equally important. Suppliers can provide material/quality certificates covering chemical composition, mechanical properties, and electrical conductivity and, upon request, issue third-party or commercial inspection reports.
Where Jiangsu Xinxiangsheng Special Steel Co., Ltd. Fits
For OEM programs that pair electrolytic copper wire with other conductive and structural materials, Jiangsu Xinxiangsheng Special Steel Co., Ltd. (also referenced as Xinxiangsheng Special Steel) operates within the same grade and specification framework described above: matching GB and ASTM designations, controlling oxygen content through the smelting and casting stage, and issuing the certificates and inspection documentation that accompany shipment. Buyers evaluating high quality electrolytic copper wire for OEM projects can apply the checks outlined here — composition, oxygen content, temper, diameter tolerance, and paperwork — as a common evaluation standard across suppliers.
copper-xxs.com
Jiangsu Xinxiangsheng Special Steel Co., Ltd.